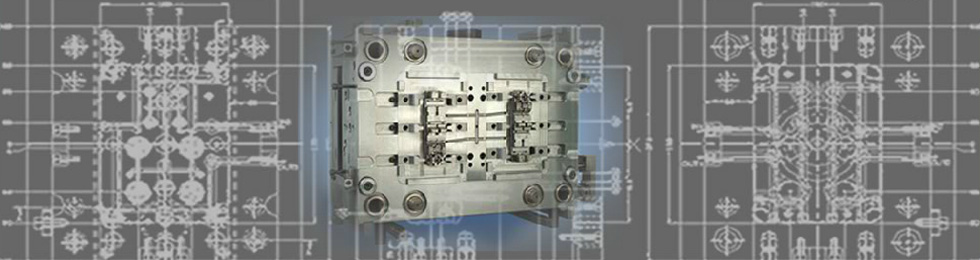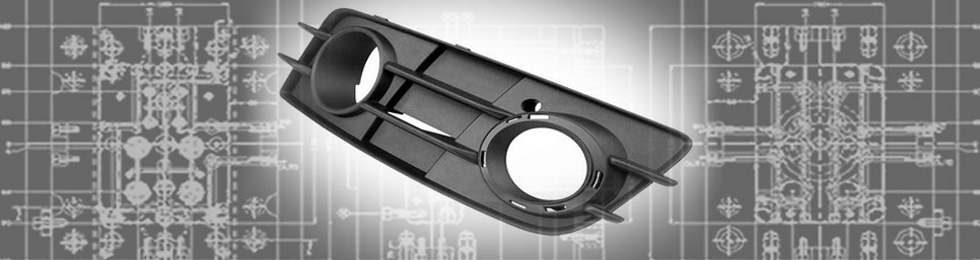
UTTMould handled mold design, manufacturing, trials, small-batch trial production and export for a top-and-bottom plastic housing project. The mold was accepted and delivered. The project illustrates how tooling specifications, trial samples and inspection activities connect within an export mold project.
| Item | Project details |
|---|---|
| Components | Top and bottom plastic housings |
| Specified cavity arrangement | 4+4 cavities |
| Material specified for molding | PS Shock STYRON A-TECH 1200 |
| Specified shrinkage allowance | 0.60% |
| Destination listed in the tooling specification | France |
| UTTMould scope | Design, manufacturing, mold trials, small-batch trial production and export |
| Project outcome | Mold accepted and delivered |
Material and shrinkage values above are tooling specification inputs, not measurements of the finished parts. Customer names and internal project identifiers are omitted.
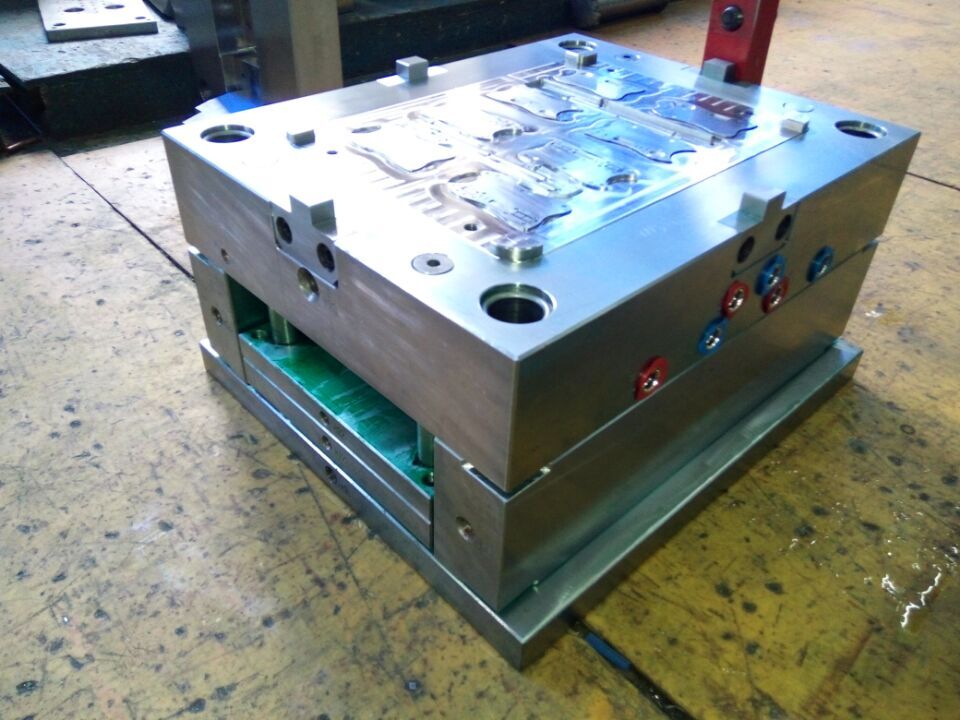
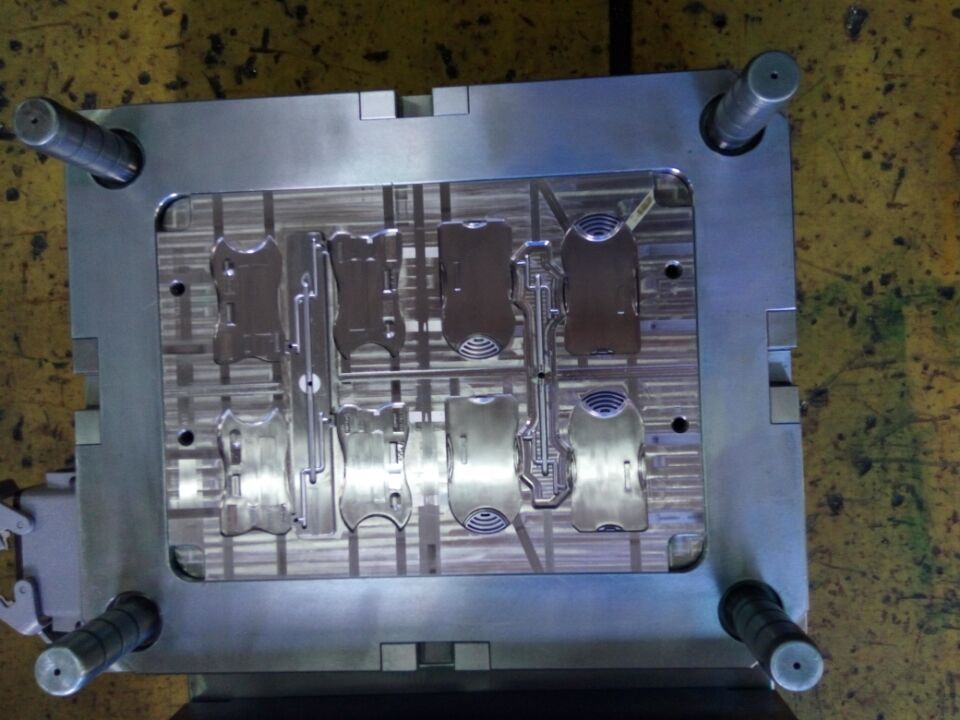
The project specification calls for a combined mold with four top-housing cavities and four bottom-housing cavities. It records requirements for the molding material, shrinkage allowance, gating, ejection, surface finish and machine compatibility.
For buyers sourcing an injection mold from China, a specification of this kind helps define the requested tool before manufacturing. Design inputs should remain distinct from acceptance evidence: a shrinkage allowance informs tool design, while inspection records document the results obtained from molded samples.
UTTMould's confirmed scope covered the mold from design and manufacturing through trials and small-batch trial production. The project photographs include the tool installed on a molding machine and samples of the two housing components.
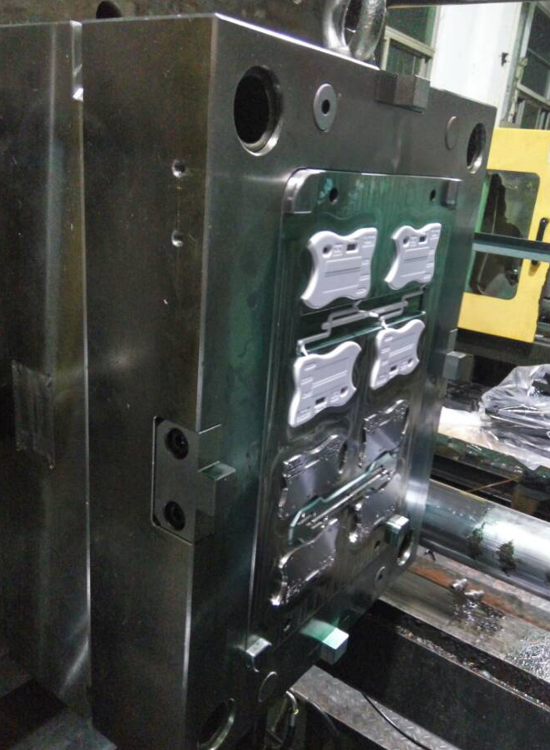
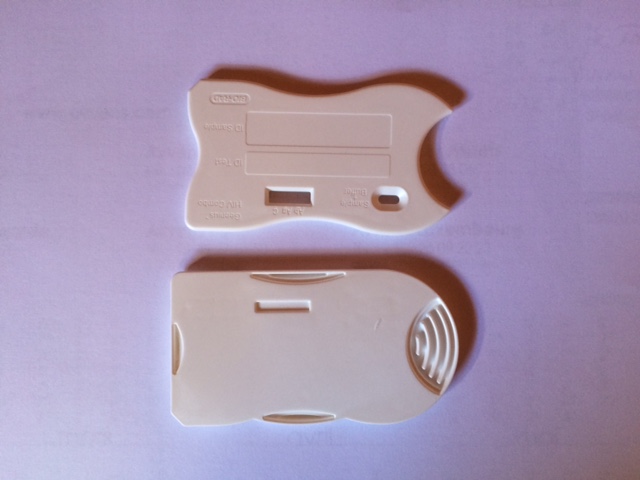
This scope links the tool build with the first molded parts, rather than treating mold manufacture as a standalone handover. Buyers planning a similar project can review UTTMould's mold manufacturing services and mold trials and injection molding production.
The project records include a digital indicator with a contact probe positioned on a molded housing sample.
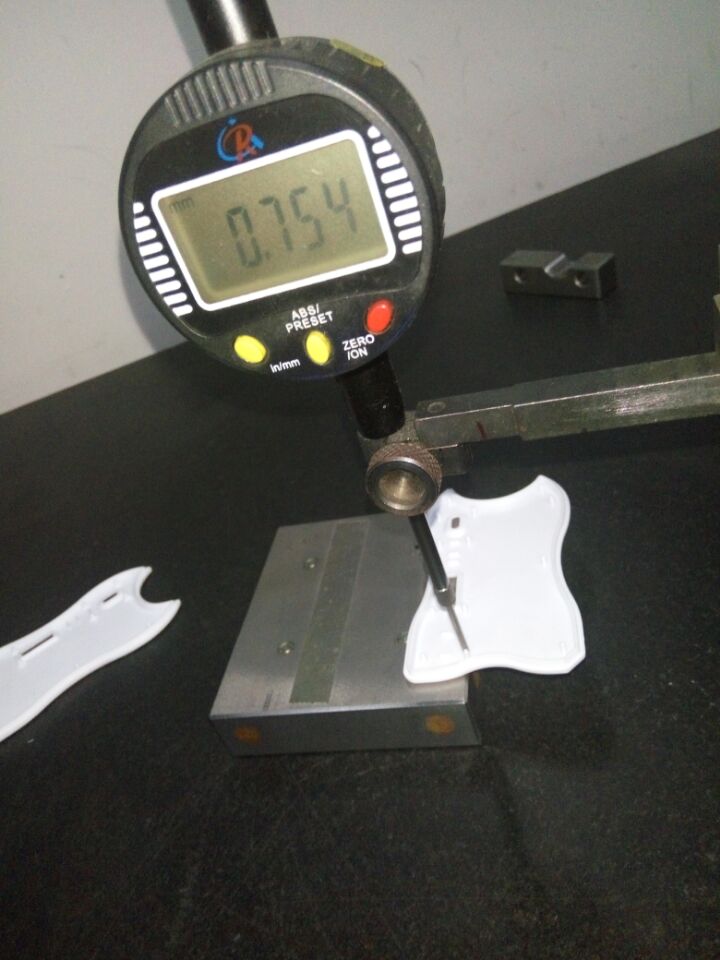
For a documented dimensional check, the reading needs to be associated with the measured feature, reference setup, drawing requirement and permitted variation. The photograph does not establish those details, so it is presented as a record of inspection activity rather than a claim about wall thickness, flatness or dimensional capability.
UTTMould confirmed that the mold was accepted and delivered after its work on the project. Actual cycle time, accumulated mold life and production yield are not reported here because supporting operating records are not included in the published case materials.
See the quality-control overview when defining the inspection and acceptance scope for a new mold.
For a top-and-bottom housing mold, prepare:
Contact UTTMould for a project-specific mold quotation. Share the drawings and production plan so that the tooling, trial-production and export scope can be reviewed together.
Follow Us: 


Copyright © 2026 UTTMould All Rights Reserved Sitemap XML Quality Inspection Checklist Injection Mold Guide